Key takeaways
- Establish common maintenance processes across sites while allowing approved changes for local equipment, operating conditions, and safety needs.
- Use shared asset identifiers, failure codes, work-order fields, and status definitions to make maintenance records easier to compare.
- Define each stage of the work-order lifecycle, from reporting a fault to verifying completed work.
- Use common KPI definitions for MTBF, MTTR, preventive maintenance compliance and maintenance backlog.
- Connect frontline teams with central operations through digital forms, mobile checklists, approvals, evidence capture, and reporting.
A maintenance team at one plant may close a work order as soon as a repair is complete. At another site, the same job may need supervisor approval before closure. A third location may record the equipment fault under a different failure code.
Each team may be following its own version of the company’s maintenance process. When the head office reviews performance, the records do not tell the same story.
This becomes harder to manage as industrial organisations expand across plants, facilities and regions. Sites may develop separate maintenance routines, asset registers, work-order formats and reporting practices. Some differences are needed because equipment, operating conditions and safety requirements vary. Others come from local workarounds or systems that were introduced at different times.
Organisations need a common maintenance process that still gives each site room to manage its equipment and daily operations.
To standardize maintenance workflows across multiple sites, companies need shared rules for reporting maintenance needs, planning jobs, assigning work, recording execution and verifying completion. They also need reliable data to compare maintenance activity across locations.
This guide covers the steps involved, the processes that need common rules and the role digital platforms can play in supporting maintenance teams.
Why maintenance workflows become inconsistent across sites
A company may have a central maintenance policy, but that does not mean every facility follows the same process.
One plant may use a computerised maintenance management system (CMMS), while another relies on spreadsheets and paper work orders. A facility acquired several years ago may still use its original asset naming system. Maintenance managers may have introduced different approval steps, priority levels and reporting formats.
Over time, these differences affect how maintenance work is managed.
Consider an organisation with three manufacturing plants. All three maintain similar production equipment, but their teams record equipment failures differently:
- Plant A categorises a pump failure as a mechanical fault.
- Plant B records it as an equipment breakdown.
- Plant C uses a local code based on the affected production line.
The teams may be describing the same type of problem. However, the central maintenance team cannot easily group the records, compare recurring failures or identify patterns across locations.
Other differences may include:
- Different definitions of high-priority maintenance work.
- Preventive maintenance schedules managed separately at each site.
- Work orders closed without a shared verification process.
- Incomplete records of labour, materials and repair activities.
- Different versions of maintenance instructions in use.
- Limited visibility into overdue jobs and unresolved defects.
These gaps make it harder to review maintenance performance across the organisation. They can also affect planning, resource allocation and the sharing of effective practices between sites.
Before introducing a common standard, organisations need to identify where these differences occur and which ones are required by local operating conditions.
1. Map the existing maintenance workflows at every site
Start by finding out how maintenance work takes place at each location.
A central maintenance policy may describe the planned process. Workers may also follow steps that have developed through experience. Some help them manage local conditions. Others add delays or lead to inconsistent records.
Map the full maintenance process, from the moment a problem is reported to the point when the work is completed and reviewed.
| Workflow stage | What to examine |
|---|---|
| Work identification | How are equipment problems, inspection findings and maintenance requests reported? |
| Review and prioritisation | Who reviews requests, and how are priority levels assigned? |
| Planning | How are labour, tools, materials, permits and job requirements identified? |
| Scheduling | Who assigns work, and how are shift availability and production schedules considered? |
| Execution | How do technicians access instructions and record completed work? |
| Completion | What information is required before a work order can be closed? |
| Review | How are completed jobs, recurring failures and overdue work assessed? |
Speak with maintenance managers, planners, supervisors and technicians. Review actual work orders and maintenance records instead of relying only on written procedures.
Select one common maintenance activity, like servicing a pump or inspecting a conveyor, and compare how each site handles it.
Check the information collected, approval steps, job assignments, execution instructions and completion requirements.
The aim is to identify which differences are needed and which can be replaced with a shared process.
2. Decide what should be standardised and what should remain site-specific
A multi-site maintenance programme needs common rules and controlled local changes.
Applying identical procedures to every facility may seem straightforward, but industrial sites do not operate under identical conditions. Equipment age, production demands, environmental exposure, operating hours, and safety requirements can differ.
Two plants may operate the same type of pump. One may run continuously in a high-temperature environment, while the other operates intermittently under different process conditions. Their maintenance schedules may need to differ.
The organisation should establish common rules for managing work. Maintenance strategies can then reflect the condition and operating requirements of individual assets.
| Standardise across sites | Allow controlled local variation |
|---|---|
| Asset identification principles | Maintenance frequency based on asset condition and operating conditions |
| Work-order stages and status definitions | Technician assignments and shift arrangements |
| Required information in maintenance requests | Local access and operating restrictions |
| Minimum work documentation | Site-specific safety procedures and permits |
| Approval and escalation responsibilities | Approved changes based on equipment or process requirements |
| KPI definitions and reporting methods | Resource allocation based on local availability |
| Procedure ownership and revision control | Additional checks required by local laws or risk assessments |
This distinction matters when developing preventive maintenance programmes.
A common maintenance process can define how preventive tasks are planned, assigned, recorded and reviewed. It does not need to impose the same maintenance interval on every asset of a particular type.
Maintenance frequency should account for manufacturer recommendations, operating conditions, equipment history, criticality and the organisation’s maintenance strategy.
The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide describes four maintenance approaches: reactive, preventive, predictive and reliability-centred maintenance. It provides technical guidance on each approach and its application. The right mix depends on equipment criticality, failure patterns, downtime costs and available resources.
The organisation should standardise how maintenance decisions are made and recorded while allowing those decisions to reflect each site’s requirements.
3. Build a common asset and maintenance data structure
A shared workflow cannot solve the problem if every site records maintenance information differently.
A common data structure gives the organisation one way to identify equipment, classify failures and review maintenance activity.
This also supports the wider principles of asset management. ISO 55000:2024, Asset management: Vocabulary, overview and principles, sets out key terms and principles for managing assets across their life cycles and linking asset management with organisational objectives.
Establish consistent asset identification
Every asset should have a unique identifier that can be recognised across the organisation’s maintenance records.
The asset hierarchy should follow a shared structure. One possible arrangement is:
Site → Building or Area → Production Line → System → Equipment → Component
The exact structure depends on the organisation and its assets. Every site should follow the agreed method for naming, identifying and locating equipment.
This helps teams distinguish between similar assets and connect maintenance history to the correct equipment.
Agree on failure and work-order categories
Organisations should also establish shared definitions for:
- Equipment failure types.
- Failure causes.
- Maintenance activity categories.
- Work-order priorities.
- Planned and unplanned maintenance.
- Work-order status.
- Reasons for delays.
- Completion and verification requirements.
Consider two plants that report repeated motor overheating.
If one records the problem as an electrical fault and the other records it as a mechanical breakdown, central reporting may fail to identify the recurring issue. A shared failure classification helps maintenance teams review similar events using the same terms.
Define the information required in every work order
A common work-order template should capture the information needed to plan, execute and review maintenance work.
Depending on the task, this may include:
- Site and asset identifier.
- Description of the reported problem.
- Work priority.
- Assigned technician or team.
- Required tools and materials.
- Relevant work instructions.
- Safety requirements and permits.
- Work performed.
- Readings, observations, and supporting evidence.
- Completion status and verification details.
Not every field needs to be mandatory for every job. A routine lubrication task does not need the same information as a major equipment repair.
Define the minimum set of shared information, then add task-specific fields where required.
The result should be a maintenance record that teams can understand and review, regardless of which site created it.
4. Standardise the complete maintenance work-order lifecycle
A work order does more than record that a maintenance task exists. It connects the people, information and decisions needed to complete the job.
A shared work-order process should define what happens at each stage and who is responsible.
Maintenance management research describes work management through stages that include identification, planning, scheduling, execution, completion and analysis. The terms may differ across organisations, but the main steps remain similar.
Consider a pump that develops abnormal vibration at a manufacturing facility.
Identify the maintenance requirement
An operator notices unusual vibration during a routine equipment check.
The operator raises a maintenance request with the asset identifier, location, observation, and relevant reading. A photograph or other supporting evidence may help the maintenance team assess the reported condition.
The organisation should define the minimum information needed to submit a useful request.
Review and prioritise the request
A maintenance supervisor reviews the request and decides what action is needed.
The organisation should establish shared priority definitions. An issue that affects safety or creates an immediate production risk needs a different priority from a minor defect that can be addressed during planned maintenance.
Priority rules should account for risk assessments, equipment criticality and operating requirements.
Plan the job
Before assigning the task, the planner or maintenance team identifies the resources and preparation required.
This may include:
- Technician skills and authorisations.
- Tools and spare parts.
- Equipment isolation requirements.
- Permits and safety precautions.
- Required technical instructions.
- Estimated labour and job duration.
A consistent planning process reduces the risk of technicians reaching a job without the information or resources needed to complete it.
Schedule and assign the work
The job is assigned based on its priority, resource availability, technician competence, and the site’s operating schedule.
A shared scheduling process helps managers see which jobs are planned, overdue, deferred, or waiting for resources.
Local teams may still need to adjust assignments around shift patterns, production requirements and site access.
Execute and record the work
The technician carries out the task using the relevant procedure and safety controls.
The maintenance record should capture the work performed, observations, readings, parts used where required, and any unexpected conditions.
For a pump repair, this may include the initial vibration reading, the component inspected, the corrective action and the reading recorded after the repair.
This creates a record of the work performed, rather than simply showing that the work order was marked complete.
Verify and close the work order
The organisation should define what counts as completion.
For some routine tasks, the technician’s completion record may be enough. Other jobs may need supervisor review, quality verification or confirmation that the equipment is ready to return to service.
The work order should retain the required completion information and list any outstanding actions.
Review the maintenance record
Completed work should become part of the asset’s maintenance history and wider performance analysis.
The maintenance team can review recurring faults, repair duration, repeat work and other patterns to decide where further investigation is needed.
When every site follows a comparable process, the organisation has a more reliable basis for reviewing maintenance activity across its facilities.
5. Standardise work instructions without ignoring local safety requirements
A common work-order process does not guarantee that technicians perform each task in the same way.
They also need access to the right instructions, equipment information and safety requirements.
For organisations with several locations, procedures can be hard to manage. Different sites may use outdated documents, locally changed instructions or knowledge passed between experienced technicians.
A controlled digital work instructions process should cover these areas.
Common task requirements: Establish the standard steps, checks, and expected results for repeatable maintenance activities.
Document ownership: Assign responsibility for approving and maintaining each procedure.
Version control: Make it clear which version is current and prevent workers from using outdated instructions.
Access at the point of work: Help technicians retrieve the right procedure when they need it. In areas with limited connectivity, the chosen system should support offline access.
Completion evidence: Define what workers need to record to show that the task was completed.
Feedback and revision: Give technicians a way to report unclear instructions, missing steps, and recurring problems.
Safety procedures need particular attention.
The US Occupational Safety and Health Administration’s 29 CFR 1910.147, Control of Hazardous Energy (Lockout/Tagout), covers servicing and maintenance activities where unexpected equipment energisation, start-up or release of stored energy could cause injury. It requires an energy-control programme that includes procedures, employee training and periodic inspections.
This is a US regulatory reference. Organisations operating in other countries must follow the occupational safety laws and standards that apply to their sites.
A central procedure may set out the organisation’s approach to energy isolation. The actual instructions must still account for the equipment and site conditions.
A common digital checklist cannot replace a machine-specific lockout/tagout procedure, permit requirement or site risk assessment.
Standard work instructions should include the right local controls. People responsible for safety and maintenance should review any changes.
6. Create a controlled process for local exceptions
No maintenance procedure can cover every condition a technician may face.
A spare part may be unavailable. A machine may have unexpected damage. Site access restrictions may affect the planned work. An operating condition may require the maintenance team to stop and reassess the task.
If workers have no approved way to handle these situations, they may create informal workarounds.
Over time, these workarounds can become undocumented local procedures.
Define how exceptions should be handled. A controlled process should answer four questions:
- When can a deviation be made? Define the conditions under which the standard procedure may need to change.
- Who can approve it? Establish the authority required for each type of deviation.
- What must be recorded? Capture the reason, decision, person responsible, and any additional controls.
- When should the standard be reviewed? Track repeated exceptions that suggest the original procedure needs an update.
A technician may discover that a replacement component listed in the work order is unavailable. The job may need to be deferred, or an alternative component may need to be assessed.
The decision should follow the organisation’s engineering and approval requirements. The maintenance record should explain why the original plan changed.
This gives central teams visibility into local conditions while allowing technicians to respond to changes safely.
It also gives the organisation information it can use to improve procedures across its facilities.
7. Use common maintenance KPIs to compare performance across sites
A multi-site maintenance dashboard is useful only when the information behind it can be compared.
Suppose one plant reports high preventive maintenance compliance while another reports a lower figure. Before deciding that the first site performs better, management needs to understand how each location calculates compliance.
Do both sites use the same definition of a completed task? Are deferred work orders treated in the same way? Are overdue jobs included consistently? Do the reporting periods match?
Without shared definitions, the figures may appear comparable while measuring different things.
The Society for Maintenance & Reliability Professionals (SMRP) publishes Best Practices, Metrics & Guidelines, which covers more than 70 maintenance and reliability metrics. Each metric includes a definition, objective, formula, component terms, and supporting information.
Organisations can use established industry references when developing their maintenance scorecard.
Useful measurement areas include:
| Metric | What it helps assess |
|---|---|
| Mean Time Between Failures (MTBF) | Operating time between recorded failures for an asset or group of assets |
| Mean Time to Repair (MTTR) | Average time taken to restore equipment after a failure, based on the organisation’s chosen measurement method |
| Preventive maintenance compliance | Whether scheduled preventive maintenance work is completed within the agreed period |
| Maintenance backlog | The amount of maintenance work awaiting completion, based on an agreed definition |
| Planned versus reactive work | How maintenance activity is divided between planned tasks and work triggered by failures or unexpected conditions |
| Rework | Whether completed maintenance tasks need to be repeated or corrected |
Document the calculation method and data requirements for each measure.
MTTR can use different time boundaries. An organisation must decide whether it measures active repair time, elapsed time from failure to restoration, or another defined interval. Each site should use the same method.
The same care is needed with preventive maintenance compliance. Sites should agree on which work orders are included, how due dates are set, and how approved deferrals are treated.
It also helps to separate two types of measurement:
Process adoption: Are sites using the agreed work-order stages, recording required information and following approval steps?
Maintenance performance: Are reliability, repair, and maintenance-planning results changing over time?
The first shows whether the standard is being used. The second helps assess whether the maintenance strategy is producing the expected results.
Neither measure should be read on its own. A site with older equipment or more demanding operating conditions may have different reliability results, even when it follows the same maintenance process as other locations.
8. Roll out the standard across sites in phases
Once the organisation has agreed on the common workflow, data requirements and governance rules, it needs a practical implementation plan.
Introducing a new process across every site at once can disrupt daily work. It may also reveal problems that were not found during the design stage.
A phased rollout gives teams time to test the process under actual operating conditions.
Select representative pilot sites
Choose locations that reflect different operating conditions, equipment types, and levels of digital maturity.
A pilot at only the most advanced facility may not reveal the difficulties faced by sites with older systems or limited connectivity.
Agree on the common requirements
Bring maintenance managers, planners, supervisors, technicians, and safety personnel together to review the proposed standard.
Agree on asset identification, work-order stages, required information, approval rules, and performance definitions.
Configure and test the workflow
Set up the forms, instructions, responsibilities, notifications, and reporting requirements.
Test routine work and exceptions. A process that works for a planned inspection may need changes before it can support an urgent breakdown.
Train the people who will use it
Training should cover the actual maintenance process, along with the software.
Technicians need to know what information to record. Supervisors need to understand how to review and approve work. Planners need to know how the standard affects scheduling and resource allocation.
Review the pilot and make adjustments
Collect feedback from the people performing and managing the work.
Check for incomplete records, unnecessary approval steps, unclear instructions, and repeated exceptions. Correct these issues before extending the standard to other locations.
Expand in stages
Introduce the revised workflow to additional sites using lessons from the pilot.
Keep the main requirements consistent while allowing approved local differences.
Review performance on an ongoing basis
Assign responsibility for maintaining procedures, reviewing exceptions, checking data quality and monitoring adoption.
Review whether the standard still matches the organisation’s equipment, processes and operating requirements.
A standard that is introduced once and never reviewed can become outdated, just like the local procedures it was meant to replace.
9. How digital platforms support standardised maintenance workflows
Technology can help organisations put a common maintenance process into daily use.
Different systems support different parts of maintenance work.
A CMMS or enterprise asset management (EAM) system supports asset records, maintenance planning, work orders and maintenance history. Maintenance management software can help teams organise these activities and track work across assets.
A digital frontline workflow platform helps workers access task instructions, complete mobile checklists, capture evidence, obtain approvals and submit information from the field.
These systems may work together, depending on the organisation’s existing technology and integration needs.
When evaluating maintenance workflow software, organisations operating across multiple sites should check whether it supports:
- Consistent digital forms and workflow steps.
- Shared information requirements across locations.
- Mobile access for technicians and operators.
- Photo, video, reading and observation capture.
- Approval and escalation processes.
- Offline work and synchronisation when connectivity returns.
- Reporting across sites, assets and work categories.
- Integration with existing CMMS, ERP, MES or other operational systems.
The same requirements matter when assessing maintenance operations software. Managers need to see how work moves across sites, where jobs are delayed and whether teams are recording the information needed for review.
A maintenance workflow platform should support the agreed process and give frontline teams a practical way to complete their work. Organisations should also assess how it connects with existing systems before selecting a platform.
How Telepresenz SmartOPS™ supports frontline maintenance workflows
Telepresenz SmartOPS™ is an AI-powered field operations platform with CMMS capabilities. It supports maintenance planning and scheduling, asset tracking, digital workflows, mobile checklists, approvals, evidence capture, reporting and remote assistance.
For organisations working across multiple facilities, these capabilities can help connect maintenance processes with the people carrying them out.
For example, digital workflows can guide workers through defined task steps and capture the information required for review. Photos, videos, observations, and other job records can provide supporting evidence. Offline functionality helps field teams continue recording work in areas with limited connectivity, with data syncing when a connection returns.
See How Digital Workflows Support Industrial Maintenance
SmartOPS can also connect with wider enterprise systems, including ERP, MES, SCADA and IoT platforms, depending on the integration and deployment.
The aim is to give operations and maintenance teams a more consistent way to manage and review frontline work while working with their existing operational environment.
Honeywell digitised field operations across 17 plants
Honeywell managed operations across 17 heat and chill plants. Before the deployment, operators recorded equipment readings and system parameters on paper. Staff later transferred the information into Excel, while physical logbooks supported shift handovers.
This process added to the reporting workload and made it harder for managers to review operational information across the facilities.
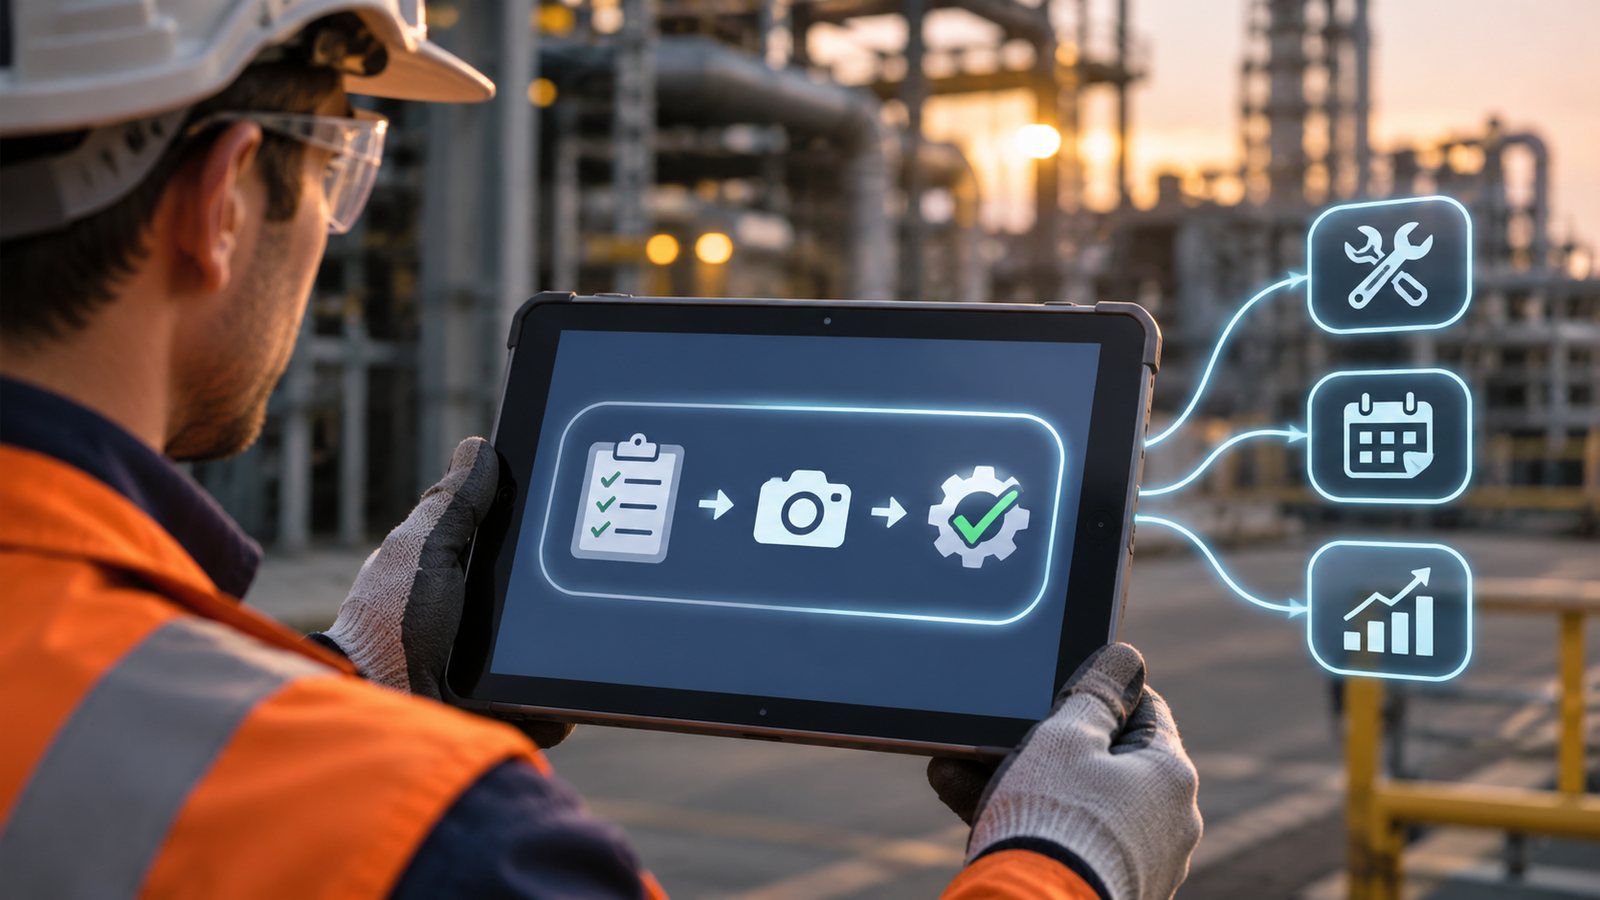
At Telepresenz, we used SmartOPS™ to digitise field rounds. Operators recorded readings, comments, and photographs on mobile tablets. Entries included timestamps and geotags, while supervisors could review information through a central dashboard.
- 90% reduction in manual reporting time.
- More than one million operational records digitised within eight months.
- Digital traceability of inspection records across the operation.
The Honeywell deployment shows how a digital workflow can replace manual field records and make operational information easier to review across multiple facilities.
Read the Honeywell Fort Liberty case study.
Standardising maintenance workflows across multiple sites requires shared processes for reporting work, planning and scheduling jobs, recording execution, verifying completion and reviewing results.
Organisations also need consistent asset information, maintenance classifications and KPI definitions. These help managers compare records from different facilities and identify where changes may be needed.
The standard should still account for differences in equipment condition, operating requirements and site-specific safety controls. Local teams need an approved way to manage exceptions and suggest changes.
When process rules, information requirements and ownership are in place, organisations gain a more reliable view of maintenance activity across their facilities. Digital platforms can support this process by connecting agreed workflows with the people doing the work.
FAQs
What does maintenance standardisation mean across multiple sites?
Maintenance standardisation means establishing common processes, data definitions, responsibilities and performance measures across an organisation’s facilities. It helps ensure that maintenance work is requested, planned, executed, documented, and reviewed using a consistent framework, while allowing approved variations for local operating conditions.
Which maintenance processes should every site follow?
Most multi-site organisations should establish common rules for asset identification, maintenance requests, work-order prioritisation, planning, scheduling, execution records, completion verification, approvals and performance reporting. The exact procedures may vary according to equipment, risk and operating requirements.
How do you standardise work orders across different facilities?
Start by defining common work-order categories, priority levels, status definitions, mandatory information, and approval requirements. Map the existing processes at each facility, identify unnecessary differences, and introduce a shared workflow. Test it with maintenance teams before extending it across the organisation.
Should all sites follow the same preventive maintenance schedule?
No. Organisations can standardise how preventive maintenance is planned, assigned, documented and reviewed without imposing identical maintenance intervals on every asset. Schedules should account for equipment condition, operating hours, criticality, manufacturer guidance, maintenance history and site conditions.
How can organisations compare maintenance performance across plants?
They need common KPI definitions, calculation methods, reporting periods and data requirements. Measures such as MTBF, MTTR, preventive maintenance compliance and maintenance backlog can support comparisons when sites calculate them consistently. Differences in equipment and operating conditions should also be considered when interpreting results.
Can maintenance workflows be standardised across different CMMS platforms?
Yes, at the process level. Organisations can define common work-order stages, information requirements, approval rules and performance measures even when sites use different systems. However, data exchange, reporting and workflow integration may require additional configuration or system integration. A shared process does not automatically make different systems interoperable.
Written by
Indu Tolia
Founder and CEO of Telepresenz
She leads the company’s work to help industrial organizations make frontline work safer, more connected, and more efficient through technology.
Connect with Indu Tolia on LinkedIn